Explore our high-performance vibration isolation components, engineered with proprietary vulcanized bonding technology, aerospace-grade aluminum forgings, and application-tuned elastomeric compounds.
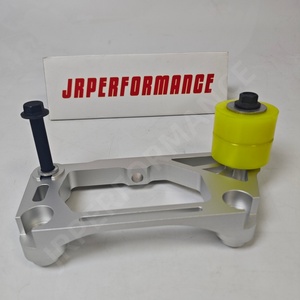
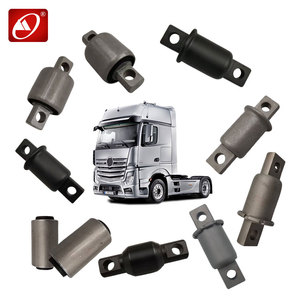
Vibration isolation in dynamic chassis, powertrain, and driveline assemblies requires careful tuning of static-to-dynamic stiffness ratios, viscoelastic loss factors, and boundary layer molecular adhesion.
The interface between metallic inner/outer sleeves and elastomeric matrices is the typical point of mechanical vulnerability. We implement automated multi-stage aqueous degreasing, micro-grit zinc phosphating, and Chemlok adhesive polymeric dip coating to achieve 100% rubber failure during destructive peel testing.
Uncontrolled acoustic resonance creates vehicle harshness. Our polymer compounding targets an ideal loss factor (tan δ 0.12 - 0.28) and minimizes dynamic hardening at high frequencies (up to 400 Hz), mitigating both road shock amplitude and subframe acoustic transfer into the cabin.
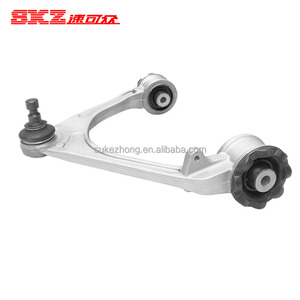
For applications such as differential carriers, subframe mounts, and sway links, dimensional stability is maintained through 5-axis CNC machining and cold-forged 6061-T6 aerospace aluminum alloys or normalized structural steel, preventing fatigue cracking and pin deflection under full cornering load.
Different automotive mounting locations experience distinct thermal, environmental, and cyclical stress regimes. We compound raw elastomers to exact OEM specifications.
| Polymer Base | Operating Temp Range | Tensile Strength (MPa) | Oil & Solvent Resistance | Primary Industrial Application | Lifecycle Benchmark |
|---|---|---|---|---|---|
| Natural Rubber (NR Grade 1) | -45°C to +80°C | ≥ 22.5 MPa | Moderate (ASTM Oil #3: >60% Swell) | Control arm bushings, strut top mounts, leaf spring eyes | 3.5M Fatigue Cycles |
| EPDM (Peroxide Cured) | -40°C to +135°C | ≥ 16.0 MPa | High Ozone / Glycol / UV Immunity | Subframe isolators, radiator vibration dampers, exhaust hangers | 4.0M Fatigue Cycles |
| Hydraulic Fluid NBR / HNBR | -35°C to +140°C | ≥ 19.0 MPa | Superior (Hydrocarbon / ATF Immersion) | Hydro-bushings, active engine mounts, differential snubbers | 5.0M Fatigue Cycles |
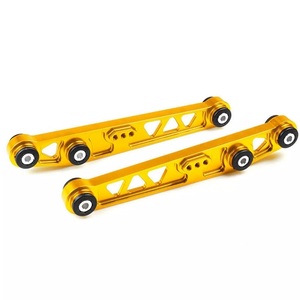
| Polyurethane (Cast Millable) | -30°C to +95°C | ≥ 32.0 MPa | Exceptional Abrasion & Shear | Motorsport trailing arms, heavy mining truck suspension links | High Load Deflection |
The global automotive aftermarket and Tier-1 supply chain are undergoing structural realignment. Procurement executives are shifting away from fragmented trading middlemen to directly auditable manufacturing facilities capable of vertical integration.
Electrification (EV) and high-torque hybrid powertrains impose unprecedented low-frequency vibrational loads, accelerating the need for advanced damper engineering across all suspension links.
From raw compound formula synthesis to end-line coordinate measuring machine (CMM) inspection, we operate a fully closed-loop industrial facility designed to eliminate fitment error and field returns.
We do not outsource critical molding or vulcanization processes. Our factory hosts 80+ hydraulic vacuum vulcanizing presses and an internal tooling shop that cuts down mold development times from months to weeks.
Fitted with high-precision multi-axis CNC machines and cold-forging presses, our facility produces high-strength aluminum control arms and differential support brackets that exceed OEM dimensional repeatability tolerances.
Every batch of raw elastomer is tested for rheometer cure curve, Mooney viscosity, and tensile elongation. Finished dampers undergo tri-axial dynamic fatigue endurance tests, salt spray corrosion tests (1000+ hrs), and bond peel testing.
Key answers addressing custom tooling, minimum order quantities (MOQ), quality certifications, rubber formulation, and shipment logistics.
Whether you require direct catalog SKU wholesale, complete chassis bushing programs, or custom CNC-machined anti-vibration mount engineering, our engineering and export team is ready to assist your procurement program.