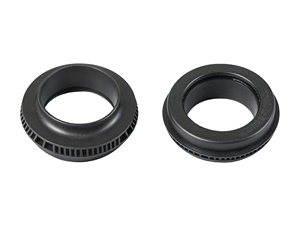
Shock Absorber Mount Rubber Bushing Suspension Support Bearing Car Replacement Part
High-density dynamic damping compound engineered to insulate strut impacts and sustain axial deflection loads.

Engineered to absorb severe torsional deflection, eliminate road harmonic resonances, and maintain exact wheel geometry under extreme dynamic loads.
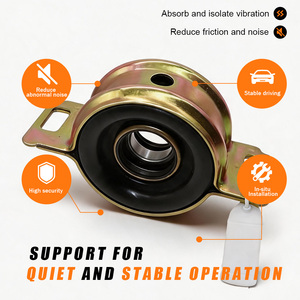
Analyzing elastomeric shear modulus, adhesive interphase integrity, and dynamic fatigue cycles across severe off-highway and heavy transport environments.
Radius arm bushings (often classified interchangeably with suspension trailing link and strut rod bushings) represent the definitive structural pivot bridging an axle housing or carrier assembly directly to the chassis frame. Unlike conventional passenger car suspension links, radius arms on commercial vehicles, 4WD platforms, and heavy pickups must counteract catastrophic longitudinal braking torque, multi-axis torsional articulation, and severe driveline acceleration forces simultaneously. When an axle twists under maximum torque, the elastomeric core undergoes non-linear multiaxial strain.
At our dedicated Thailand production facilities, our elastomer compounding formulation strictly circumvents the premature micro-fissuring and high compression sets standard in cheap secondary market bushings. By integrating custom-engineered Natural Rubber (NR) blends with optimized cis-1,4-polyisoprene ratios and synthetic polybutadiene compounds, we achieve an exceptional tensile threshold (>22 MPa) paired with optimal hysteresis dissipation. This dynamic absorption eliminates mechanical cab shudder without transmitting harsh high-frequency road vibrations through the chassis rail.
| Mechanical & Material Property | NISTO OEM/ODM Specification | Standard Generic Aftermarket | Functional Impact |
|---|---|---|---|
| Base Elastomer Compound | Premium Virgin NR / Synthetic Copolymer Blend | Recycled Rubber / High Clay Filler Loading | Fatigue life extended to >500,000 cycles without structural hardening. |
| Rubber-to-Metal Bonding | Chemlok® Multi-Coat Adhesive with Automated Degreasing | Single-layer primer, manual dip application | Zero interfacial delamination under extreme high-angle torsion. |
| Sleeve Material & Finish | Seamless Cold-Drawn DOM Steel, Phosphated & Anti-Corrosion Plated | Welded seam ERW pipe, low-grade zinc wash | Eliminates inner sleeve crushing during high-torque bolt tightening. |
| Shore A Durometer Accuracy | Strictly Calibrated 65 ± 3 Shore A | Unregulated 60 to 80 Shore A Variance | Preserves calculated vehicle roll centers and factory steering track. |
| Thermal Operational Range | -40°C to +120°C Continuous Service | -15°C to +80°C Service Threshold | Guaranteed resilience in arctic freeze or continuous desert hauling. |
How fleet electrification, predictive asset lifecycles, and direct-factory supply chains are reshaping commercial procurement strategies.
The expansion of electric light commercial vehicles (e-LCVs) generates immediate low-end torque profiles far exceeding traditional internal combustion engines. This instant acceleration exerts immediate angular shear forces onto radius arm assemblies. Tier-1 buyers and distributors are migrating to stiffened dual-compound elastomeric designs capable of isolating battery pack high-frequency mass resonances without fatiguing under recurring peak-torque launches.
Importers and international brand owners are rapidly abandoning multi-tiered intermediaries in favor of vertically integrated factories that maintain in-house tool design, CNC turning, and elastomer compounding. Direct engineering transparency provides auditable vulcanization process controls, significantly decreases standard MOQ friction, and shortens SKU catalog development turnarounds down to 25–35 operational days.
High-payload fleets require dynamic fluid-filled hydraulic radius arm bushings to handle variable load damping. We engineered specialized cavity coring within our mold architectures, enabling the production of fluid-decoupled or internal voided designs. This delivers low dynamic stiffness during low-amplitude highway coasting and high progressive resistance during heavy off-road suspension articulation.
Combining Thailand’s domestic natural rubber supremacy with automated manufacturing discipline to guarantee zero line defects.
We exercise end-to-end sovereignty across every step of production. From primary polymer compound mixing to multi-cavity hot vulcanization, zero operations are sub-contracted, ensuring absolute consistency from batch to batch.
Our expansive production tooling infrastructure provides verified cross-reference coverage across 31 vehicle marques, including Toyota, Ford, Nissan, Isuzu, Mitsubishi, Honda, and heavy commercial vehicle platforms like Hino.
Based in the epicenter of the global rubber belt, our plant maintains ready-ship stock inventories on thousands of popular items. This guarantees low lead times, competitive ocean logistics, and streamlined customs execution.
Every single radius arm bushing is produced to tight OE engineering parameters. Inner steel sleeves are CNC finished and surface-treated to avoid galvanic corrosion, seizing, or bore galling during pressing.
Addressing engineering specifications, custom mold commissioning, material hardness verifications, and global ordering minimums.
The most frequent failure mode is rubber-to-metal bond separation caused by continuous axial shear stresses and exposure to road salts and engine lubricants. We prevent this by utilizing shot-blasting surface etching on all inner and outer steel sleeves, followed by robotic multi-coat adhesive application (Chemlok®). This creates a molecular-level covalent bond between the metal and cured rubber that exceeds the shear strength of the elastomer itself.
Yes. As an OEM/ODM specialist, our engineering department regularly executes complete custom reverse engineering and mold fabrication. If you supply an original CAD file (STEP/IGES), 2D specification drawing, or physical bench sample, our mold-making center produces pilot tooling and vulcanization test samples within 20 to 30 working days, backed by complete CMM dimensional inspection and dynamic durometer reports.
Consistency in durometer ratings is maintained by mixing our raw compounds in tightly regulated internal mixers (Banbury mixers) governed by computerized temperature, pressure, and time parameters. Every masterbatch undergoes rheometer testing before release to vulcanization lines, ensuring that your parts consistently meet a tight 65 ± 3 Shore A (or custom requested) specification across millions of units.
For catalog items where tooling already exists in our 9,485+ SKU database, our standard minimum order quantity starts as low as 200–500 units per line item depending on the bushing dimensions. For newly developed OEM/ODM custom compounds and tooling, standard pilot production runs require 500–1,000 units. Typical lead-times run between 30 to 45 days after deposit and final technical sample validation.
Our production standards mandate seamless cold-drawn steel or precision DOM (Drawn Over Mandrel) tubing for high-stress radius arm and trailing link bushings. Welded tubing possesses structural seam weakness that can fracture or distort out-of-round during heavy hydraulic press-fitting into suspension eyes. Seamless sleeves ensure complete structural rigidity and uniform radial interference fits.
Partner with a verified manufacturer in Thailand. Whether you require standard OEM replacement inventory cross-referenced by part number or bespoke high-damping poly/rubber compounds for demanding heavy-duty applications, our engineering sales division is on standby.
Send an Inquiry